5s
+1
Submission successful!

|
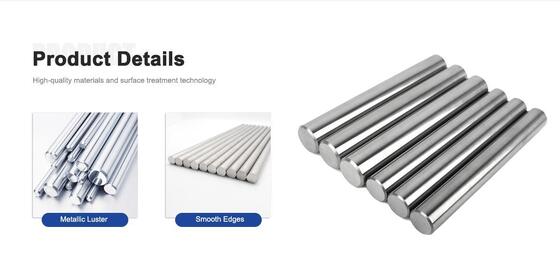
| Brand Name: | DLX |
| Model Number: | Nimonic 80A |
| MOQ: | 10kg |
| Payment Terms: | L/C,D/A,D/P,T/T,VTB |
| Supply Ability: | 1200 tons per month |
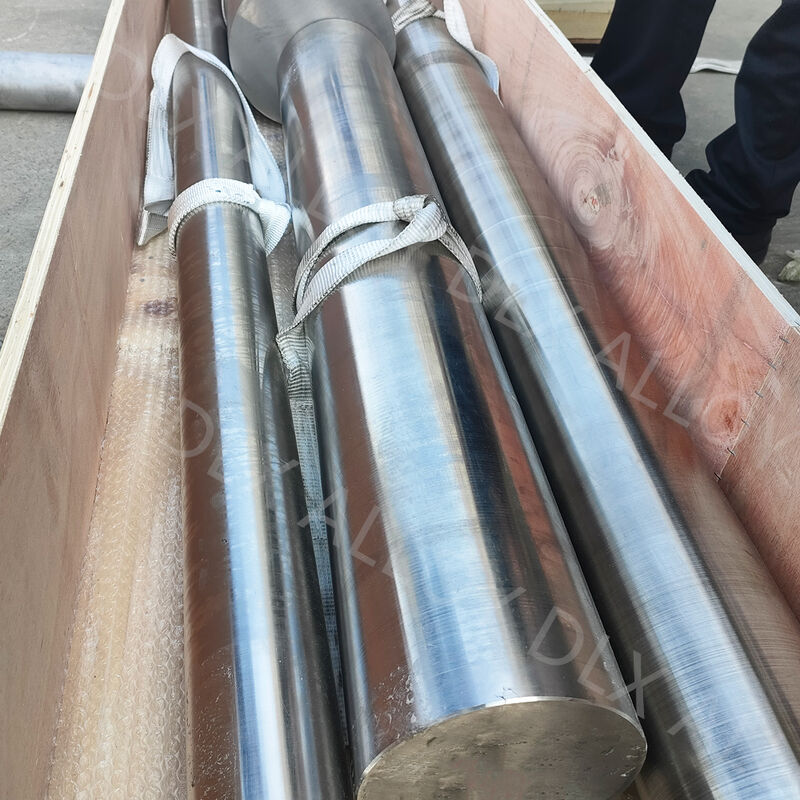
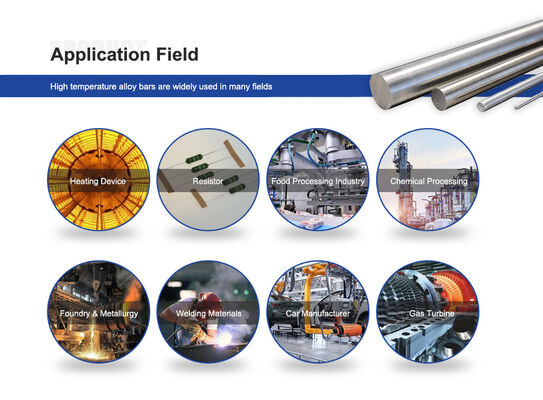
Engineered for extreme thermal stability and superior creep-rupture resistance up to 815°C, our vacuum-melted, precision ground Nimonic 80A round bar delivers uncompromising mechanical integrity for gas turbine rotor blades, marine exhaust valves, and critical nuclear bolting.
Our Nimonic 80A round bar delivers superior resistance to high-temperature oxidation and cyclic thermal fatigue. The alloy forms a protective, adherent chromium oxide layer at elevated operating temperatures, effectively preventing surface degradation under severe oxidizing combustion gases.
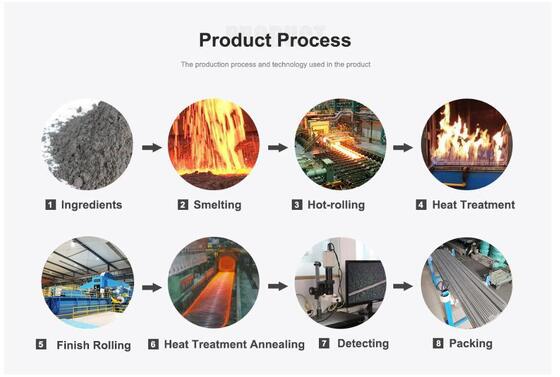
Through comprehensive in-house hot forging, solution annealing, precision straightening, and centerless grinding processes, every Nimonic 80A round bar achieves uniform gamma prime (γ′) phase distribution. This optimized microstructure guarantees exceptional structural stability under prolonged mechanical stresses at red-hot operating conditions.
Key metallurgical highlights include:
| Element | Content (wt%) | Function in Nimonic 80A Matrix |
|---|---|---|
| Nickel (Ni) | Balance (~68.0 - 74.0%) | Austenitic matrix, thermal stability & oxidation resistance |
| Chromium (Cr) | 18.00 – 21.00% | High-temperature corrosion and oxidation barrier |
| Titanium (Ti) | 1.80 – 2.70% | Primary gamma prime (γ′) precipitation hardener |
| Aluminum (Al) | 1.00 – 1.80% | Secondary precipitation strengthening & oxidation resistance |
| Iron (Fe) | ≤ 1.50% | Controlled residual matrix balance |
| Carbon (C) | 0.04 – 0.10% | Grain boundary carbide stabilization |
| Cobalt (Co) | ≤ 2.00% | Solid solution strengthening |
| Silicon (Si) | ≤ 0.80% | Melting deoxidizer |
| Manganese (Mn) | ≤ 0.40% | Hot workability enhancement |
| Sulfur (S) | ≤ 0.015% | Strictly minimized trace impurity |
| Property Parameter | Metric Value | Imperial / Notes |
|---|---|---|
| Density | 8.19 g/cm3 | 0.296 lb/in3 |
| Melting Range | 1320−1365∘C | 2410−2490∘F |
| Specific Heat (20∘C) | 448 J/(kg⋅K) | 0.107 Btu/(lb⋅∘F) |
| Thermal Conductivity (20∘C) | 12.3 W/(m⋅K) | High thermal dissipation efficiency |
| Electrical Resistivity (20∘C) | 1.24 μΩ⋅m | Matrix stability |
| Magnetic Permeability (20∘C) | <1.001 | Non-magnetic in all conditions |
| Mechanical Parameter | Room Temperature (20∘C) | High Temperature (700∘C) |
|---|---|---|
| Tensile Strength (Rm) | ≥1050 MPa | ≥720 MPa |
| Yield Strength (Rp0.2) | ≥680 MPa | ≥520 MPa |
| Elongation (A5) | ≥20% | ≥15% |
| Reduction of Area (Z) | ≥25% | ≥20% |
| Hardness (Brinell / Rockwell) | 300−360 HBW / 32−38 HRC | Fully heat-treated state |
| Stress Rupture Life | — | ≥100 hours at 700∘C/400 MPa |
A: Unlike standard stainless steels that lose yield strength rapidly above 550°C, the Nimonic 80A round bar is reinforced through coherent γ′ (Ni3(Al, Ti)) precipitate formation during aging. This microstructure allows it to maintain high tensile strength (>700 MPa) and superior creep resistance up to 815°C, preventing blade elongation under centrifugal force.
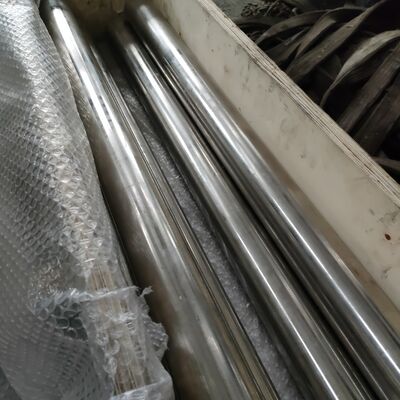
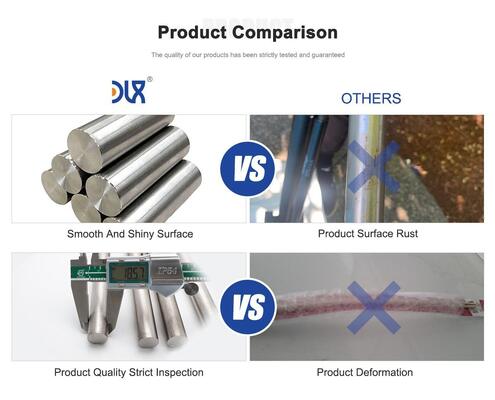
A: Our round bars are processed via automated centerless grinding machines, achieving precision tolerances within ISO h7/h8/h9 grades and surface roughness of Ra≤0.4 μm. This guarantees high circularity and straightness, minimizing tool chatter during downstream machining.
A: The standard two-stage heat treatment consists of:
A: All round bars undergo 100% immersion or contact Ultrasonic Testing (UT) combined with Eddy Current Surface Testing to ensure zero internal shrinkage, microporosity, or longitudinal crack defects.
A: Standard stocked bar sizes can be dispatched within 7–10 days. Custom forgings and tailored ground diameters typically require 3–4 weeks. All rods are coated with anti-rust protective oil, plastic capped at ends, vapor-barrier wrapped, and secured in reinforced fumigated wooden crates.


 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 中文
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski