5s
+1
Submission successful!

|
| Brand Name: | DLX |
| Model Number: | Nickel-Clad Copper Strip C10200 |
| MOQ: | 5kg |
| Payment Terms: | L/C,D/A,D/P,T/T,VTB |
| Supply Ability: | 500 tons per month |
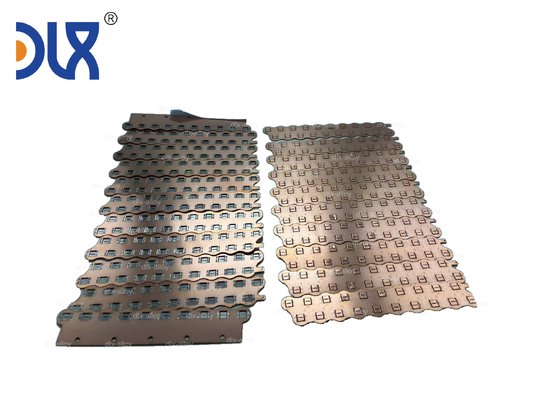
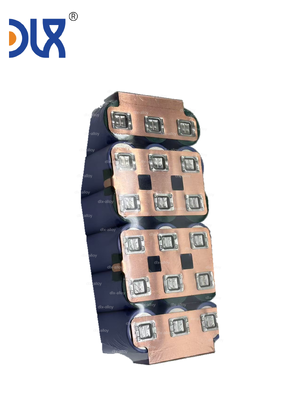
High-purity C10200 (TU1) oxygen-free copper strip metallurgically clad with pure nickel on single or double sides, specifically engineered for 21700 lithium-ion cylindrical battery interconnects and contact tabs. Delivers ≥100% IACS core electrical conductivity with superior anti-corrosion properties and spatter-free laser weldability.
DLX Alloy's C10200 nickel-clad copper strip (Cu-Ni composite transition ribbon) is an advanced bimetal conductor developed for high-rate 21700 cylindrical battery cell tabs and current collectors. Utilizing high-purity C10200 / TU1 Oxygen-Free Electronic (OFE) copper as the core substrate and pure nickel as the cladding layer, this material achieves near-zero electrical transfer loss while eliminating the contact oxidation and weld-spatter drawbacks of bare copper. Fully compliant with ASTM B152 and GB/T 5231 industrial standards, available in precision strip thicknesses from 0.10 mm to 0.40 mm with tight slitting width tolerances down to ±0.005 mm.

The 21700 cylindrical battery format is widely utilized in high-density electric mobility, portable power stations, and cordless industrial tools due to its high continuous discharge ratings (15A–35A per cell). Under rapid charge and discharge cycles, traditional pure nickel connecting tabs generate excessive internal resistance (R ≈ 9.6 μΩ·cm), causing Joule heating and thermal runaway risks in compact multi-cell enclosures.
Bare copper offers superior electrical conductivity but presents severe manufacturing hurdles: high reflectivity to standard 1064 nm fiber laser beams, rapid oxidation under ambient humidity, and galvanic corrosion when in direct contact with steel battery cans.
DLX Alloy's C10200 (TU1) nickel-clad copper strip solves this industry bottleneck through solid-state continuous roll-bonding. The C10200 oxygen-free copper core provides maximum thermal and electrical dissipation (≥ 100% IACS), while the continuous metallurgical nickel skin provides an impervious corrosion barrier and high laser absorptivity for clean, high-speed spot and fiber laser welding on 21700 positive caps and negative cans.
| Technical Parameter | Core Layer (C10200 / TU1 OFC Copper) | Outer Layer (Ni200 / Pure Nickel) | Clad Composite Strip Performance |
|---|---|---|---|
| Chemical Composition | Cu ≥ 99.95%, O ≤ 0.001% (OFC) | Ni ≥ 99.60%, C ≤ 0.05% | Metallurgically Bonded (Zero Peeling) |
| Applicable Standards | ASTM B152, GB/T 5231 | ASTM B160, GB/T 2072 | ISO 9001:2015, RoHS & REACH Certified |
| Total Thickness | 0.08 mm – 0.35 mm | 0.01 mm – 0.03 mm (Per Side) | 0.10 mm – 0.40 mm (Custom Ratios) |
| Slit Width & Tolerance | Per Drawing | Per Drawing | 3.0 mm – 120.0 mm (Tolerance: ±0.01 mm) |
| Electrical Conductivity | ≥ 100% – 101% IACS | 22% – 25% IACS | ≥ 88% – 94% IACS (Depending on Ratio) |
| Resistivity at 20°C | ≤ 0.01700 μΩ·m | ~ 0.09600 μΩ·m | 0.0183 – 0.0210 μΩ·m |
| Tensile Strength (Rm) | 210 – 270 MPa (Annealed Soft) | 380 – 480 MPa | 250 – 330 MPa (Annealed / 1/4 Hard) |
| Elongation (A₅₀) | ≥ 35% | ≥ 25% | ≥ 28% |
| Vickers Hardness (HV) | 55 – 70 HV | 100 – 130 HV | 65 – 85 HV |
| Cladding Layer Ratio | 80% – 90% Base Core | 10% – 20% (Single/Double Side) | Standard 1:8:1 or Customized |
Oxygen-Free C10200 Core for Ultra-Low Resistance: Utilizing C10200 (TU1) copper with oxygen content below 10 ppm eliminates hydrogen embrittlement risks during welding and maintains ≥ 88%–94% composite IACS conductivity.
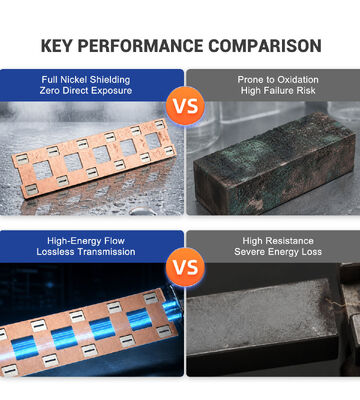
Corrosion-Resistant Metallurgical Nickel Barrier: The defect-free outer pure nickel layer isolates the copper core from moisture, electrolyte vapours, and galvanic oxidation, maintaining low interfacial contact resistance throughout extended battery lifecycles.
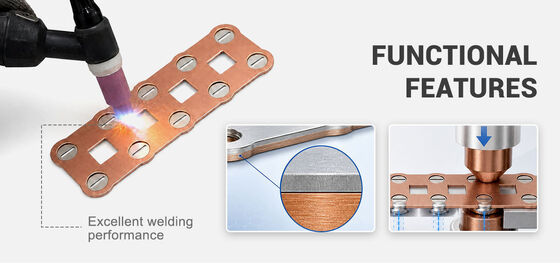
Spatter-Free Laser & Ultrasonic Weldability: Enhances 1064 nm fiber laser energy coupling, enabling low-power welding without burn-through, spatter, or cell seal degradation on 21700 battery caps.
Atomic Diffusion Bonding (Zero Delamination): High-pressure hot-rolling creates an atomic-level metallurgical interlock capable of undergoing 180° tight-radius bending and repetitive high-speed stamping without separation.
High-Precision Burr-Free Slit Edges: Rotary shear edge conditioning guarantees burr heights under 0.005 mm, preventing short-circuit risks in tight cylindrical battery cell arrays.
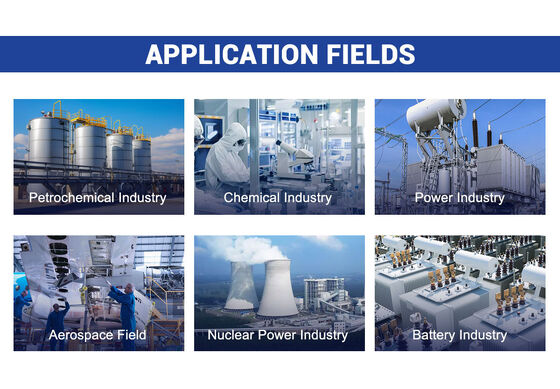
21700 High-Drain Li-ion Battery Packs: Series and parallel current-collector tabs for high-output power tools, cordless vacuum cleaners, and high-performance e-bikes.
Commercial & Residential Energy Storage Busbars: Modular interconnect strips for 21700-based micro-ESS, portable solar generators, and UPS backup power banks.
Electric Vehicle & Light EV Battery Arrays: Battery module busbars engineered to carry sustained high continuous current while minimizing parasitic resistance losses.
Battery Protection Boards (BMS) Connection Strips: Direct nickel-to-PCB solderable transition ribbons for seamless integration between BMS monitoring circuits and battery terminals.
High-Power Battery Welding Discs & Contact Plates: Pre-formed custom stamped bridge plates and terminal pads for automated pack assembly lines.
20+ Years Specialty Alloy & Clad Metal Expertise: DLX Alloy is an ISO 9001:2015 certified manufacturer specializing in precision bimetallic transition strips, high-purity copper, and nickel alloys for the global energy storage sector.
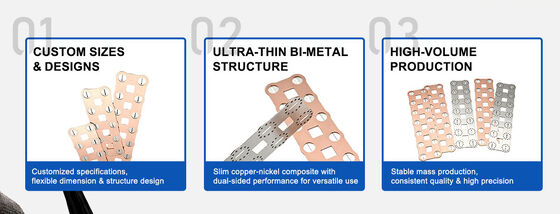
Custom Cladding Architecture & Thickness Ratios: Full flexibility to engineer single-sided clad, double-sided symmetric clad, or selective zone-plated strips matching your specific impedance and stamping requirements.
100% In-House Mechanical & Electrical Verification: Every production lot is tested for eddy-current conductivity, interfacial shear adhesion, 180° reverse-bend ductility, and dimensional uniformity.
Micro-Precision Slitting Capabilities (± 0.005 mm): Advanced CNC slitting lines deliver flat, camber-free ribbon coils with burr-free edges optimized for automated high-speed stamping feeders.
Direct Factory Supply & Fast Sample Prototyping: Rapid turnaround with sample lead times of 5–7 working days for custom widths and thicknesses, accompanied by complete mill test certificates (MTC).
Q1: What makes C10200 (TU1) oxygen-free copper superior to standard C11000 copper for battery tabs?
A: C10200 (TU1) is an Oxygen-Free Electronic (OFE) grade copper with oxygen content strictly controlled below 0.001% (10 ppm). Unlike C11000 (which contains trace cuprous oxide), C10200 is completely immune to hydrogen embrittlement during high-temperature thermal cycling and resistance welding, ensuring maximum joint ductility, higher thermal conductivity, and superior fatigue resistance.
Q2: How does the corrosion resistance of nickel-clad copper compare to bare copper in battery packs?
A: Bare copper readily forms copper oxide and green patina when exposed to ambient moisture or trace electrolyte fumes, increasing contact resistance over time. DLX Alloy's nickel cladding acts as a dense, inert barrier that resists oxidation and galvanic corrosion, maintaining stable micro-ohm electrical conductivity across the entire 21700 pack lifespan.
Q3: Is this C10200 nickel-clad strip suitable for automated high-speed laser welding?
A: Yes. Pure copper has an optical reflectivity exceeding 90% at standard 1064 nm fiber laser wavelengths, causing erratic weld penetration and severe spatter. The outer nickel layer absorbs laser energy efficiently at lower power settings, facilitating smooth, deep-penetration weld pools directly into the 21700 steel casing without heat damage to internal cell gaskets.
Q4: What are the standard packaging and coil specifications for automated stamping machines?
A: We supply precision continuous coils wound on high-durability plastic or cardboard cores (inner diameter: 76 mm / 100 mm / 200 mm), sealed in vacuum-sealed moisture-proof aluminum foil packaging with silica gel desiccant. Custom spooling (traverse winding) is available to ensure continuous, jam-free feeding in progressive stamping dies.
Q5: Can DLX Alloy customize the nickel cladding thickness ratio for specific resistance targets?
A: Yes. While our standard configuration features a symmetrical double-sided 10%–15% nickel layer (e.g., 10% Ni / 80% Cu / 10% Ni), we can engineer custom volumetric ratios from 5% up to 25% nickel per side, or single-sided cladding according to your exact current-carrying and welding parameters.


 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 中文
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski