5s
+1
Submission successful!

|

| Brand Name: | DLX |
| Model Number: | Hastelloy C276 |
| MOQ: | 5kg |
| Payment Terms: | L/C,D/A,D/P,T/T,VTB |
| Supply Ability: | 1200 tons per month |
Hastelloy C276 is an ultra-low carbon nickel-molybdenum-chromium-tungsten alloy widely recognized as the premier solution for harsh chemical processing and high-pressure vessel fabrication. In thick-plate pressure vessel welding, uneven heat input and high restraint often cause conventional nickel filler rods to suffer from hot cracking or heat-affected zone (HAZ) corrosion sensitization.
Our Dia 2.4mm crack-resistant C276 TIG wire resolves these engineering challenges through ultra-clean vacuum induction melting (VIM) plus electroslag remelting (ESR). By maintaining trace impurities (phosphorus, sulfur, carbon, and silicon) at stringent threshold minimums, this filler wire prevents low-melting eutectic phases along grain boundaries, guaranteeing crack-free multi-pass weldments in deep groove joints.
| Technical Property | Parameter Value / Range | Engineering Benefit |
|---|---|---|
| Product Form & Diameter | Straight TIG Rod / Cut Length, Dia 2.4mm (1000mm standard) | Optimal wire feed rate and thermal input balance for 6-25mm plate |
| Base Metallurgy | Nickel-Molybdenum-Chromium-Tungsten Matrix | Universal resistance to localized pitting and crevice attack |
| Typical Chemical Composition | Ni: Bal. (~57%), Mo: 15.0-17.0%, Cr: 14.5-16.5%, Fe: 4.0-7.0%, W: 3.0-4.5%, Co: ≤2.5%, Mn: ≤1.0%, V: ≤0.35%, C: ≤0.010%, Si: ≤0.08%, P: ≤0.020%, S: ≤0.010% | Ultra-low carbon suppresses carbide precipitation during cooling |
| Melting Range | 1325°C – 1370°C | Narrow solidification range minimizes weld pool thermal shrinkage stress |
| Density | 8.89 g/cm³ | High density with zero internal micro-porosity |
| As-Welded Tensile Strength (RmRm) | ≥ 690 - 760 MPa | Matches or exceeds high-pressure vessel shell base metal strength |
| Yield Strength (Rp0.2Rp0.2) | ≥ 380 - 450 MPa | High load-bearing capacity under dynamic cyclic pressurization |
| Elongation (A5A5) | ≥ 35% - 45% | Outstanding joint ductility preventing brittle seam fracture |
| Charpy V-Notch Impact Toughness | ≥ 120 J at -196°C cryogenic conditions | Certified cryogenic and sub-zero impact resistance |
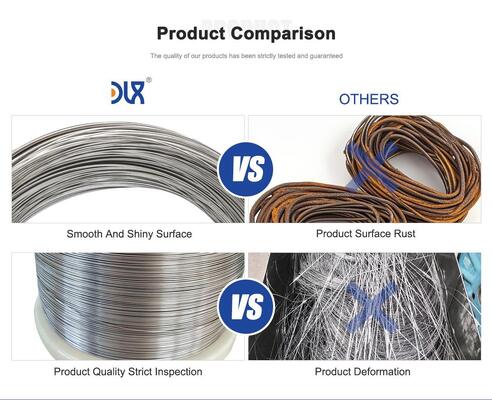
| Surface Finish & Cleanliness | Chemically brightened, grease-free, ultra-smooth draw | Zero hydrogen contamination, minimal spatter, stable TIG arc |
The specialized trace-element balancing in our 2.4mm C276 TIG rod prevents segregation of low-melting tramp elements at the solid-liquid interface during weld puddle cooling. This provides superior resistance against hot cracking, center-line solidification cracking, and crater cracking during high-amperage multi-pass welding on thick-walled pressure vessels.
Weld seams deposited by this C276 filler metal maintain homogeneous electrochemical potential across the fusion zone and HAZ. The high molybdenum (16%) and chromium (15.5%) formulation delivers exceptional defense against wet chlorine gas, hypochlorite, sulfur dioxide, hydrochloric acid, and ferric/cupric chloride pitting attack.
With carbon restricted below 0.010% and silicon below 0.08%, the deposited weld metal remains in an un-sensitized metallurgical state upon cooling. It eliminates intergranular corrosion risks at the fusion boundary, allowing direct service in aggressive chemical reactors without mandatory post-weld solution annealing.
Each wire rod is cold-drawn with sub-micron dimensional tolerance (±0.02mm) and processed through multi-stage ultrasonic degreasing. The oxide-free surface guarantees instant arc ignition, 100% X-ray radiographic inspection pass rates, and zero tungsten inclusion defects.
Used extensively in fabrication and circumferential/longitudinal butt welding of ASME-grade pressure vessels, stirred autoclaves, and hazardous waste neutralization tanks operating under elevated pressure and acidic conditions.
Ideal for precision manual and orbital TIG welding of C276 heat exchanger tubes to tubesheets, ensuring helium-leak-tight sealing under high vibration, thermal cycling, and chloride cooling waters.
Provides long-term joint survivability against acidic condensates, sulfurous sludge, and fluoride chloride mixtures in power plant wet FGD scrubber internals and ductwork liners.
Delivers NACE MR0175 compliance for downhole completion equipment, Christmas tree pipe spools, and subsea manifold systems exposed to sour crude oil and high-pressure hydrogen sulfide stress cracking.
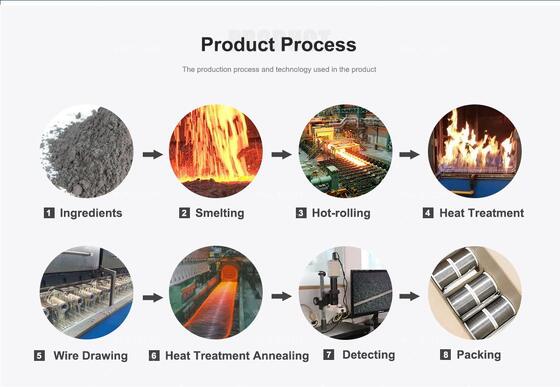
Changzhou DLX Alloy operates fully integrated manufacturing lines equipped with Vacuum Induction Melting (VIM), Vacuum Arc Remelting (VAR), and Electroslag Remelting (ESR) furnaces. Our closed-loop quality control governs every step from virgin raw ingot selection to multi-pass bright wire drawing.
With an advanced manufacturing footprint exceeding 20,000 square meters and an established monthly output exceeding 1,200 metric tons of nickel-based and specialty alloys, DLX provides reliable supply chain security, rapid order turnaround, and consistent batch-to-batch metallurgical stability for large-scale engineering projects.
Every batch of Dia 2.4mm C276 TIG wire undergoes 100% non-destructive surface inspection, spectral chemical composition verification, and destructive weld coupon mechanical/corrosion testing. Full EN 10204 Type 3.1 material test certificates and heat-number traceability are supplied with every shipment.
We offer tailored packaging including rigid moisture-proof PVC tubes, color-coded rod end stamping (C276 identification), and custom cut lengths (500mm, 1000mm, 36-inch). Our welding metallurgical engineers provide bespoke welding parameter and shielding gas optimization recommendations.
A: Dia 2.4mm (3/32") provides the optimal balance between deposition rate and precise heat input control. For pressure vessel wall thicknesses between 6mm and 25mm, a 2.4mm C276 wire delivers sufficient filler volume to ensure deep penetration while preventing excessive thermal buildup that could cause grain coarsening or distortion in the heat-affected zone.
A: Hot cracking in nickel alloy welds is primarily triggered by low-melting trace elements (P, S, B, Si) segregating to weld bead centerlines. Our C276 wire is produced via advanced ESR secondary refining, keeping total tramp impurities below 0.03%. Combined with a high-ductility matrix and narrow solidification temperature span, the weld bead easily absorbs cooling shrinkage stresses without cracking.
A: High-purity 100% Argon (minimum 99.999% purity) or an Argon-Helium mixture (e.g., 75% Ar + 25% He for higher thermal input on thick vessels) is recommended. To prevent root-pass oxidation and subsequent corrosion vulnerability, an effective purge backing with 99.999% Argon or Argon-Nitrogen mix is required until at least two fill passes are completed.
A: Yes. Hastelloy C276 filler metal is widely used for clad steel joining or welding C276 alloy to austenitic stainless steel (316L/317L) and carbon steel backings. Its high nickel-chromium-molybdenum buffer capacity accommodates dilution from iron without forming brittle intermetallic phases.
A: Standard packaging consists of 5 kg moisture-barrier PVC tubes packed into sturdy wooden export cases (1,000 kg per pallet). Minimum order quantity (MOQ) is dynamically aligned with production schedule and stock specifications, starting from 5 kg for standard stock rods.


 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 中文
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski
