5s
+1
Submission successful!

|
| Brand Name: | DLX |
| Model Number: | inconel X750 |
| MOQ: | 5kg |
| Payment Terms: | T/T,D/P,D/A,L/C,VTB |
| Supply Ability: | 1200 tons per month |
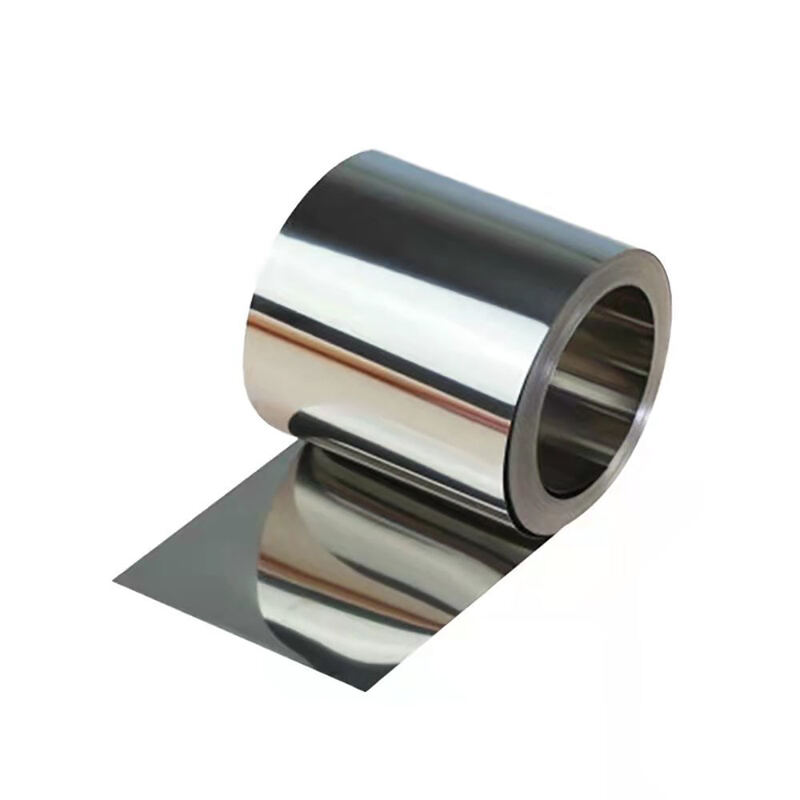
Engineered for severe deep drawing and high-temperature extrusion diaphragms, our precision annealed Inconel X750 slit strip in 0.15mm thickness delivers micron-level gauge consistency, zero-burr slit edges, and superior elastic stability up to 700°C.
High-reliability pressure sensing capsules, extrusion bursting discs, and hydraulic sensor diaphragms require raw strip materials with fine grain structures, minimal residual stress, and isotropic elongation. Precision annealed Inconel X750 slit strip in 0.15mm thickness resolves micro-cracking and localized thinning challenges by providing high initial ductility in the solution-annealed condition, followed by simple post-forming precipitation aging that achieves high yield strength and thermal stability.
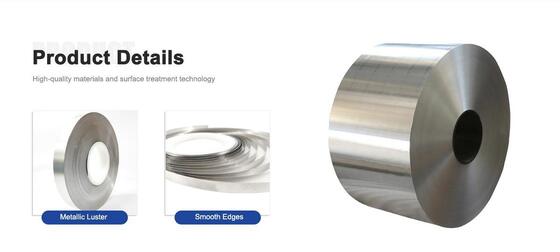
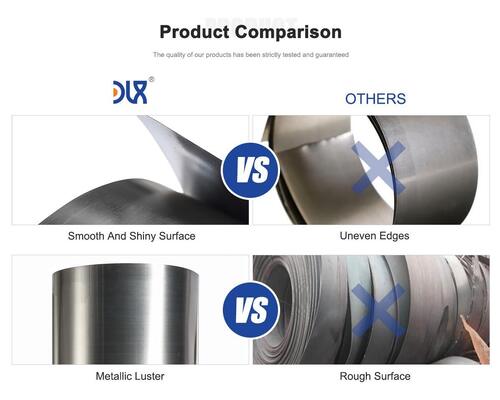
Manufactured through advanced vacuum induction melting followed by electroslag remelting, our precision slit Inconel X750 strip guarantees ultra-low inclusion counts and high microstructural cleanliness. Continuous hydrogen-atmosphere bright annealing and precision 20-high cold rolling ensure clean surface finishes and tight thickness tolerances, while dedicated rotary slitting knives provide smooth, burr-free edges essential for hermetic laser welding and automated stamping lines.
| Parameter | Standard Value / Specification Range |
|---|---|
| Material Grade | Inconel X-750 / GH4145 / Nickel-Chromium Precipitation Hardening Superalloy |
| Nominal Thickness | 0.15 mm (Custom ultra-thin foils from 0.025 mm to 2.5 mm available) |
| Thickness Tolerance | Within +/- 0.005 mm (Ultra-precision rolling down to +/- 0.003 mm on request) |
| Width Range | 5.0 mm to 350 mm (Custom slitting width tolerance +/- 0.05 mm) |
| Delivery Temper | Soft Solution Annealed (Deep Drawing / Hydroforming Grade) |
| Surface Roughness (Ra) | Smooth 2B Bright Annealed Finish, Ra <= 0.20 um |
| Edge Condition | Precision Slit Edge, Deburred Rounded Edge, Custom Edge Profiling |
| Density | 8.28 g/cm³ |
| Melting Range | 1390°C to 1430°C |
| Tensile Strength (Annealed) | 600 - 780 MPa |
| Yield Strength 0.2% Offset (Annealed) | 280 - 420 MPa |
| Elongation (A50mm) | >= 30% |
| Hardness Range (Annealed) | 150 - 190 HV / 80 - 90 HRB |
| Hardness After Precipitation Aging | 320 - 380 HV / 32 - 40 HRC |
| Operating Temperature Range | -200°C to 700°C (For spring, bellows, and diaphragm applications) |
Through controlled continuous protective-atmosphere annealing, the strip exhibits a uniform austenitic grain structure with total elongation exceeding 30%. This malleability allows multi-stage stamping, complex corrugation profiling, and hydraulic convolution without intermediate stress-relief annealing.
High-rigidity cold rolling mills maintain thickness uniformity across the entire coil width within +/- 0.005mm. Automated optical slitting lines ensure burr heights remain below 5% of nominal thickness, eliminating edge notch concentrations and extending stamping die longevity.
Upon post-forming precipitation heat treatment, uniform gamma-prime phase dispersion elevates the yield strength beyond 900 MPa, preventing thermal hysteresis, zero-point baseline drift, and permanent set under continuous thermal-mechanical cycling.
A solid-solution chromium and nickel matrix forms a dense, self-healing passivating oxide layer that resists high-temperature oxidation up to 980°C and provides superior defense against sour gas, chlorides, and petrochemical stress corrosion.
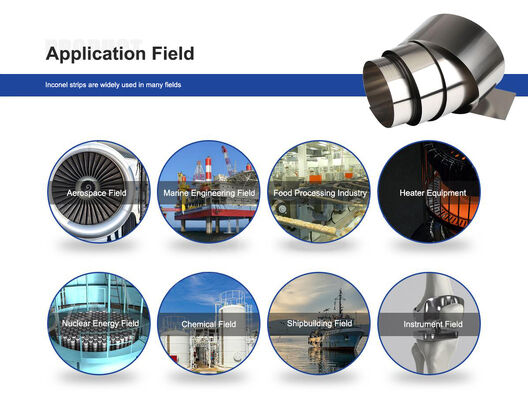
Serves as the primary corrugated diaphragm and elastic sensing core in aerospace flight instrumentation, downhole oil and gas transducers, and nuclear pressure transmitters exposed to corrosive media and extreme vibration.
Provides repeatable burst pressure thresholds and uniform plastic deflection in chemical processing rupture assemblies and high-pressure safety relief mechanisms.
Utilized in hydroformed multi-ply expansion joints, exhaust compensators, and flexible metal conduits where rapid thermal shock resistance and high cyclic fatigue life are critical.
Maintains high spring constants and structural elasticity in cryogenic aerospace valves as well as elevated-temperature turbine casing bolting systems.
DLX operates full-process production facilities encompassing vacuum induction melting, electroslag remelting, hot forging, high-precision multi-roll cold rolling, and automated tension leveling. This end-to-end metallurgical control ensures ultra-clean grain boundaries, minimal inclusion content, and total batch-to-batch repeatability.
Equipped with high-precision tungsten carbide rotary slitting lines capable of handling narrow coils down to 5.0mm width. All coils receive automated deburring, protective paper interleaving, and vacuum-sealed moisture-barrier export packaging for pristine, ready-to-stamp delivery worldwide.
With a unified production capacity of 1,200 tons per month across high-temperature and precision resistance alloy lines, DLX provides dynamic minimum order quantities tailored to strip gauge and width, supporting early-stage engineering validation as well as full-scale OEM volume manufacturing.
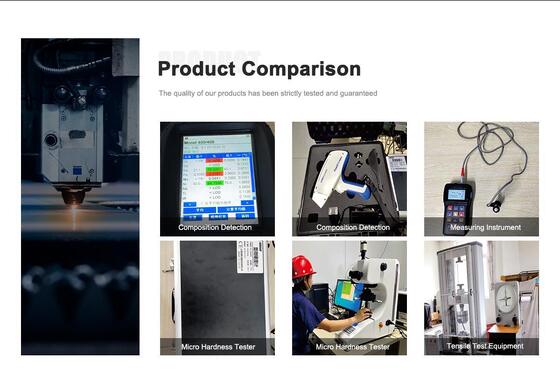
Every master coil and slit batch undergoes optical emission spectrometry, laser surface profilometry, micro-hardness gradient mapping, tensile testing, and grain size analysis prior to dispatch, accompanied by complete material verification reports.
While stainless steels suffer from mechanical hysteresis, rapid work hardening, and severe stress relaxation at temperatures above 300°C, precision annealed Inconel X750 slit strip maintains steady elastic modulus, high fatigue life, and minimal relaxation up to 700°C after precipitation aging, alongside vastly superior resistance to chloride stress-corrosion cracking.
For stamped diaphragms requiring maximum spring performance and yield strength, standard precipitation aging involves holding at 730°C (1350°F) for 16 hours, furnace cooling at 55°C per hour to 620°C (1150°F), holding for 8 hours, followed by air cooling. This develops dense gamma-prime precipitation without warping thin-gauge geometry.
We employ tungsten carbide rotary slitter knives with micron-adjusted vertical and horizontal blade clearances, coupled with in-line edge inspection. This maintains burr heights below 5% of material thickness, eliminating edge notch stresses during high-speed stamping and ensuring smooth laser weld seams.
Yes. In addition to standard tolerances, our high-precision rolling mills can achieve ultra-tight thickness tolerances within +/- 0.003mm on request. Custom cold-worked tempers (quarter-hard, half-hard, or specific tensile ranges) can also be engineered to match specific stamping tooling dynamics.
Coils are precision-wound on dedicated cores, coated with evaporative processing oil, sealed with protective edge guards, vacuum-packed with desiccant in heavy-duty VCI moisture-barrier bags, and secured in fumigated reinforced wooden crates to ensure zero surface oxidation during sea and air transit.


 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 中文
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski