5s
+1
Submission successful!

|
| Brand Name: | DLX |
| Model Number: | 1J36 |
| MOQ: | 10 kg |
| Payment Terms: | L/C,D/A,D/P,T/T,VTB |
| Supply Ability: | 1200 tons per month |
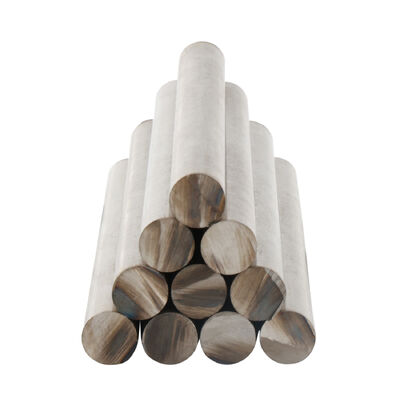
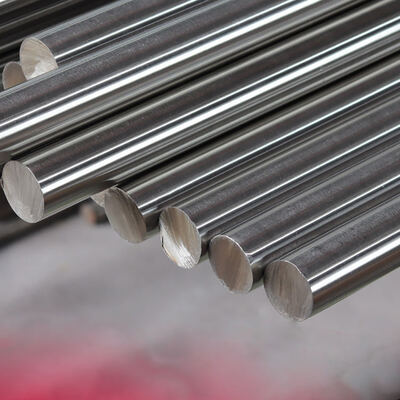
Engineered for demanding electromagnetic systems operating in corrosive, humid, and marine environments. DLX Alloy delivers premium 1J36 Ni-Fe soft magnetic alloy rods featuring high initial magnetic permeability, low coercivity, superior corrosion resistance, and precision-ground dimensional stability.

1J36 is a specialized binary nickel-iron soft magnetic alloy engineered specifically for electromagnetic applications that require structural stability and corrosion resistance without sacrificial magnetic degradation. In humid atmospheric, marine, and mildly chemical environments where conventional high-permeability soft magnetic materials are prone to oxidation and surface pitting, 1J36 maintains clean magnetic pathways and reliable flux continuity.
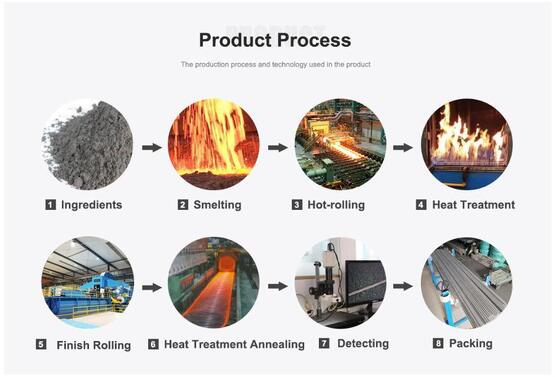
DLX Alloy produces 1J36 precision rods from ultra-pure virgin raw materials using double-vacuum melting processes. Each rod undergoes controlled hot rolling, multi-pass cold drawing, and specialized hydrogen-shielded magnetic final annealing (upon request) to deliver uniform isotropic magnetic properties along the longitudinal working axis. Our precision-straightened and centerless ground bars are tailored for high-speed CNC turning, automatic screw machining, and precision core fabrication.
| Element | Ni | Mn | Si | C | P | S | Fe |
|---|---|---|---|---|---|---|---|
| 1J36 Balance | 35.0 – 37.0 | 0.30 – 0.60 | 0.15 – 0.30 | ≤0.030 | ≤0.020 | ≤0.020 | Balance |
| Property Parameter | Metric Value | Imperial / Unit |
|---|---|---|
| Density | 8.12 g/cm3 | 0.293 lb/in3 |
| Electrical Resistivity (ρ) | 0.80 μΩ·m | 80.0 μΩ·cm |
| Curie Temperature (Tc) | 230–250 °C | 446–482 °F |
| Mean Thermal Expansion Coefficient (20–100 °C) | 1.5–4.0×10⁻⁶/K | ×10−6/°F |
| Thermal Conductivity (20 °C) | 11.0 W/(m·K) | 76.3 BTU·in/(hr·ft2·°F) |
| Magnetic Indicator | Symbol | Standard Target | Unit |
|---|---|---|---|
| Initial Permeability | μ0 | ≥3.2–4.5 | mH/m |
| Maximum Permeability | μm | ≥22.0–35.0 | mH/m |
| Coercive Force | Hc | ≤12.0–18.0 | A/m |
| Saturation Magnetic Induction | Bs | 1.25–1.35 | T |
| Parameter | Value / Range |
|---|---|
| Tensile Strength (Rm) | 460–580 MPa (Soft Annealed State) |
| Yield Strength (Rp0.2) | 220–340 MPa |
| Elongation (A5) | ≥30% |
| Hardness | ≤145 HV/≤80 HRB |
| Standard Rod Diameters | Φ1.0 mm to Φ120.0 mm (Custom cut lengths available) |
| Diameter Tolerance Options | Precision ground h7/h8, Cold drawn h9/h10 |
Unlike high-silicon iron and conventional electrical steels that oxidize readily under humid ambient conditions, the dense ~36% nickel matrix of 1J36 creates a self-passivating surface layer. This prevents magnetic degradation, surface scaling, and magnetic gap expansion in open-air and humid electromechanical assemblies.
1J36 delivers sharp magnetic responsiveness with minimal hysteresis loss. When energized, it establishes peak magnetic flux quickly; when de-energized, its ultra-low remanence ensures immediate physical detachment of moving electromagnetic armatures without residual sticking.
The balanced nickel concentration imparts low thermal expansion characteristics up to its Curie point, making 1J36 rods uniquely compatible for hermetically sealed glass-to-metal electromagnetic feedthroughs and tight-clearance magnetic actuator assemblies.
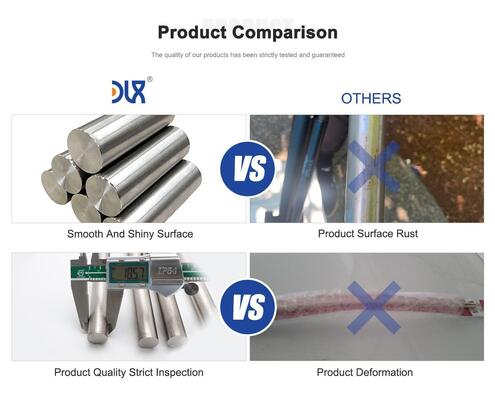
Refined vacuum melting ensures clean microstructures free of stringers or hard carbide inclusions. Our cold-drawn and centerless-ground rods deliver outstanding chip formation, high surface finish quality (Ra≤0.4 μm), and extended cutting-tool life during mass-production turning.
A1: While 1J50 and 1J85 offer higher magnetic permeability, they contain higher nickel fractions and are vulnerable to atmospheric corrosion and surface rusting in wet environments. 1J36 is specifically formulated to provide an optimum combination of moderate-to-high magnetic induction, low coercivity, and intrinsic atmospheric corrosion resistance without needing thick electroplated coatings that degrade magnetic working gaps.
A2: Yes. Severe mechanical machining, cold drawing, and stamping induce residual internal stresses that distort the crystal lattice and degrade magnetic permeability. To achieve maximum magnetic performance, finished components should undergo high-temperature vacuum or dry hydrogen magnetic annealing (1100–1150 °C followed by controlled cooling). DLX Alloy can provide pre-annealed stock or detailed heat treatment process curves for your workshop.
A3: We supply cold-drawn rods (tolerance Grade h9/h10) for general manufacturing, as well as precision centerless ground rods (tolerance Grade h7/h8) with polished surfaces (Ra≤0.4 μm) for direct feed into automatic Swiss-type and multi-axis CNC lathes.
A4: Rods are surface-oiled with anti-rust protection, bundled with moisture-proof barrier wrap, cushioned with foam separators, and packed in reinforced export wooden cases to ensure zero bending or surface oxidation during international transit.
A5: Supported by our comprehensive 1,200 tons/month factory capacity and extensive billet inventory, standard rod diameters can be dispatched within 7–10 working days, while custom precision-ground diameters and specific length cuts typically require 15–20 working days.


 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 中文
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski