5s
+1
Submission successful!

|
| Brand Name: | DLX |
| Model Number: | 1J22 |
| MOQ: | 10 kg |
| Payment Terms: | L/C,D/A,D/P,T/T,VTB |
| Supply Ability: | 1200 tons per month |
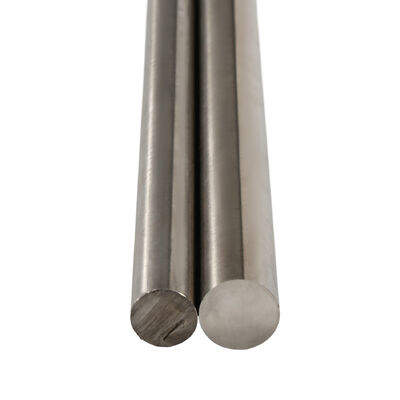
Engineered specifically for high-performance electromagnetic actuators and precision torque motor rotors, our 1J22 (Hiperco 50 equivalent) cobalt-iron-vanadium soft magnetic alloy bars deliver the highest magnetic saturation flux density available in commercial alloys—reaching up to 2.4 Tesla. Through advanced dual-vacuum melting, strict purity control, and tailored hydrogen annealing programs, we provide motor designers with maximum torque density, compact rotor dimensions, and minimal electromagnetic excitation losses.

In high-power-density electric drives, servo actuators, and direct-drive torque motors, space and weight constraints demand core materials that can carry massive magnetic flux without saturating. 1J22 (chemically balanced as 49% to 51% Co, 1.4% to 1.8% V, balance Fe, identical in performance to Hiperco 50 and Vacoflux 50) is the benchmark soft magnetic alloy engineered for these extreme electromagnetic conditions.
By combining the highest known saturation magnetization (Bs >= 2.35T to 2.4T) with high Curie temperature (980°C), our 1J22 precision bars allow electric motor engineers to increase output torque by 20% to 30% compared with conventional silicon steel cores of identical volume. Every bar is produced via Vacuum Induction Melting (VIM) followed by Electroslag Remelting (ESR), ensuring an exceptionally clean internal microstructure free from non-metallic inclusions, micro-voids, and segregated phases.
| Element | Symbol | Nominal Content (wt. %) |
|---|---|---|
| Cobalt | Co | 49.0% - 51.0% |
| Vanadium | V | 1.40% - 1.80% |
| Manganese | Mn | ≤ 0.30% |
| Silicon | Si | ≤ 0.20% |
| Carbon | C | ≤ 0.03% |
| Phosphorus | P | ≤ 0.015% |
| Sulfur | S | ≤ 0.015% |
| Iron | Fe | Balance |
| Magnetic Parameter | Symbol | Metric Value (SI) | CGS / Practical Unit |
|---|---|---|---|
| Saturation Magnetic Induction | Bs | 2.35 T - 2.40 T | 23,500 - 24,000 Gauss |
| Residual Magnetic Induction | Br | 1.40 T - 1.65 T | 14,000 - 16,500 Gauss |
| Coercive Force | Hc | ≤ 80 A/m | ≤ 1.0 Oe |
| Maximum Magnetic Permeability | μmax | ≥ 7.5 mH/m | ≥ 6,000 - 10,000 G/Oe |
| Initial Magnetic Permeability | μ0 | ≥ 1.25 mH/m | ≥ 1,000 G/Oe |
| Curie Temperature | Tc | 980 °C | 1,796 °F |
| Property | Condition / State | Value / Range |
|---|---|---|
| Density | Room Temperature | 8.20 g/cm³ |
| Electrical Resistivity | Room Temperature | 0.40 μΩ·m |
| Tensile Strength (Rm) | Annealed State | 450 - 550 MPa |
| Tensile Strength (Rm) | Cold-Worked State | 800 - 1,100 MPa |
| Elongation (A5) | Annealed State | 1.0% - 3.0% |
| Hardness | Cold Drawn / Machinable | 220 - 280 HV |
| Hardness | Final Magnetic Annealed | 180 - 220 HV |
| Parameter | Specification & Tolerances |
|---|---|
| Diameter Range | 3.0 mm - 120.0 mm |
| Standard Bar Length | 1,000 mm - 4,000 mm (Custom cut-to-length available) |
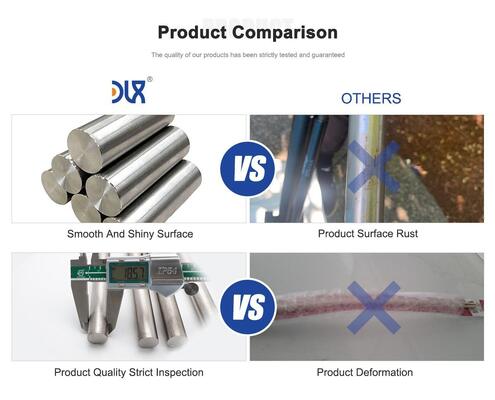
| Surface Finish | Centerless Ground (Ra ≤ 0.8 μm), Peeled, or Cold Drawn Bright |
| Diameter Tolerance | ISO h7, h8, h9, or custom precision micrometer tolerance |
| Straightness | ≤ 0.5 mm/m |
With a saturation flux density reaching 2.4 Tesla, 1J22 Hiperco 50 bars permit significantly higher air-gap magnetic loading in torque motors, enabling dramatic package downsizing or substantial torque output multiplication without increasing motor envelope dimensions.
Unlike standard silicon electrical steels that suffer sharp permeability drops beyond 1.5T, this cobalt-iron alloy maintains robust magnetic permeability across high-field operational regimes, reducing stator excitation current demand and overall copper thermal losses.
Our proprietary VIM + ESR melting process guarantees microscopic purity and homogeneous grain boundaries, preventing magnetic domain pinning, stabilizing coercive force consistency across batches, and optimizing dynamic dynamic rotor balance.
A Curie temperature of 980°C ensures that electromagnetic rotor characteristics remain stable and reliable even during continuous heavy-duty cycles and elevated motor operating temperatures up to 450°C.
Delivered in controlled cold-drawn or intermediate-annealed states, our bars provide excellent machinability for intricate rotor tooth and shaft profiling, achieving peak magnetic performance following final dry hydrogen heat treatment.
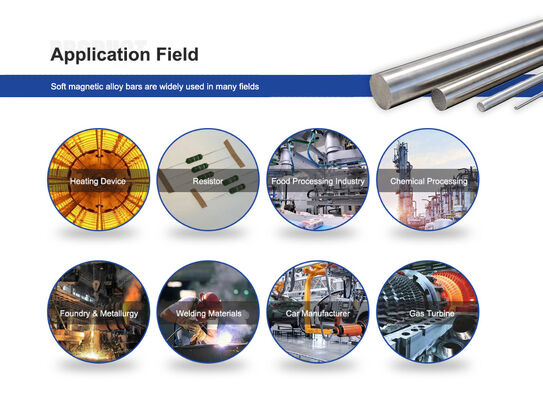
Used extensively in direct-drive servo actuators, gimbal stabilization motors, missile fin control units, and aircraft flight control surfaces requiring instantaneous maximum torque and minimum rotor inertia.
Provides compact, lightweight, and high-holding-torque rotor and stator cores for multi-axis collaborative robotic joints, precision CNC direct-drive rotary tables, and semiconductor pick-and-place equipment.
Ideal for ultra-fast magnetic switches, high-speed electromagnetic fuel injectors, and high-pressure solenoid valves where rapid magnetic flux build-up and collapse are mandatory.
Serves as flux-concentrating poles and sensor cores in precision galvanometer scanners, inertial navigation gyroscopes, and beam steering systems requiring zero magnetic hysteresis distortion.
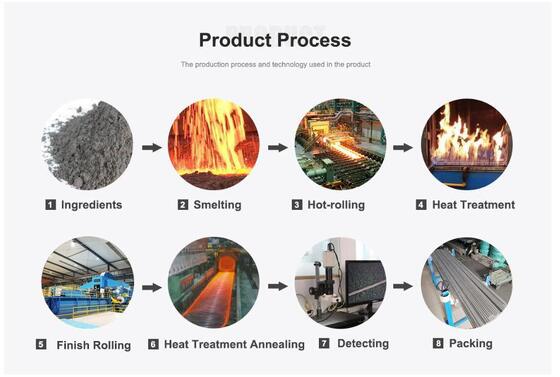
From raw material selection of ultra-pure cobalt and electrolytic iron to vacuum melting, hot forging, precision cold drawing, and centerless grinding, every manufacturing phase is tightly controlled under one roof. Our monthly processing capacity of 1,200 tons ensures reliable global volume supply with unyielding batch-to-batch consistency.
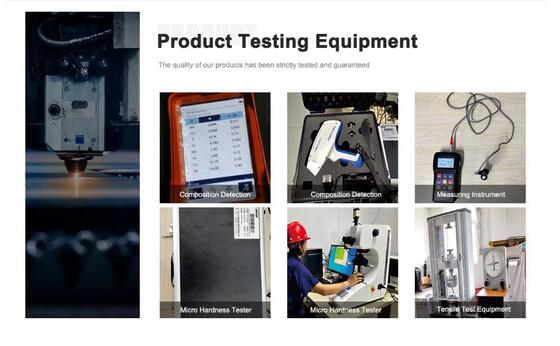
We implement full-process nondestructive testing and magnetic hysteresis loop verification on every delivery batch. Every shipment is accompanied by complete chemical composition and magnetic test documentation, ensuring your engineering team receives verified raw material data.
We recognize that soft magnetic performance is finalized during heat treatment. Our engineering team provides detailed, customized magnetic annealing parameters (temperature ramps, dry hydrogen dew points <= -60°C, and controlled cooling rates) to guarantee your machined rotor components reach maximum permeability and minimal core loss.
We support your design cycle from early prototyping to high-volume manufacturing. Standard dimensions feature low minimum order quantities starting from 5 kg, with customized dimensional tolerances delivered on compressed lead times.
1J22 Hiperco 50 has a saturation flux density of approximately 2.4T, compared to 1.5T - 1.8T for high-grade silicon steel. This allows motor designers to reduce core cross-sectional area by up to 30% while generating identical or superior electromagnetic torque, making it indispensable for aerospace and weight-sensitive direct-drive applications.
Yes. Machining introduces internal mechanical stress and dislocations that severely degrade soft magnetic properties, causing higher coercive force and reduced permeability. To restore and maximize magnetic performance, finished rotor parts must undergo final magnetic annealing in a dry hydrogen atmosphere (dew point below -60°C) or vacuum at 800°C to 840°C with carefully controlled cooling rates.
Our bars are finished using high-precision centerless grinding and precision cold drawing, offering diameter tolerances to h7 or h8 with surface roughness Ra <= 0.8 μm and straightness within 0.5 mm/m. This ensures seamless automatic bar feeder loading and high concentricity for precision rotor turning and milling.
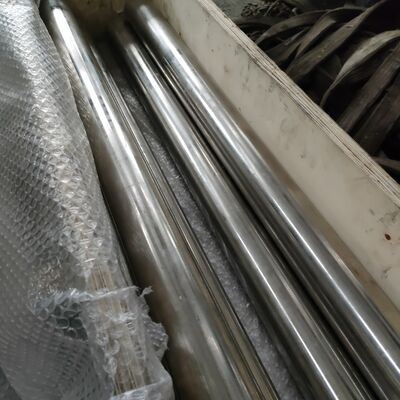
Our standard minimum order quantity is 5 kg for prototype development and sample validation. Export bars are wrapped in moisture-proof anti-rust paper, sealed in protective polymer sleeves, and secured within reinforced fumigated wooden crates to prevent surface impact, oxidation, or bending deformation during international sea or air transit.


 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 中文
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski