5s
+1
Submission successful!

|
| Brand Name: | DLX |
| Model Number: | incoloy 925 |
| MOQ: | 10kg |
| Payment Terms: | T/T,D/P,D/A,L/C,VTB |
| Supply Ability: | 1200 tons per month |
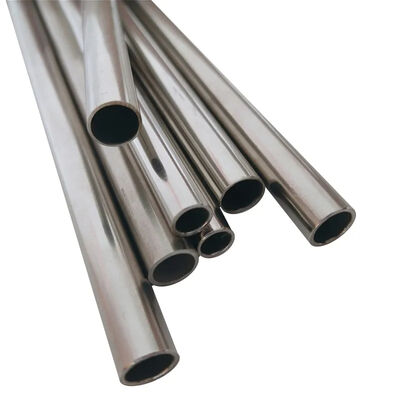
Engineered for extreme HPHT and sour gas environments, our heavy-wall (5mm–25mm) Incoloy 925 tubulars offer yield strength exceeding 120 ksi (827 MPa), micron-level CNC machining accuracy, and flawless reliability for critical subsurface flow control.
In deepwater and ultra-deep oil and gas completions, downhole safety valves serve as the final fail-safe barrier against catastrophic blowouts. The Incoloy 925 precision machined tubular component is engineered to withstand extreme borehole pressures, severe sour environments containing elevated levels of hydrogen sulfide (H2S), carbon dioxide (CO2), and high-chloride brines.
By optimizing precipitation hardening via targeted additions of titanium, aluminum, and molybdenum, our Incoloy 925 tubular components achieve high yield strength without sacrificing ductility and impact toughness. Every tubular sleeve, housing, and flow tube is precision-turned and bored with custom tooling to ensure seamless concentricity, ultra-smooth internal bores, and exact sealing surfaces required for subsurface hydraulic and electric actuators.
| Technical Parameter | Specification / Performance Benchmark |
|---|---|
| Material Grade | Precipitation-Hardenable Nickel-Iron-Chromium Alloy (Incoloy 925 / UNS N09925) |
| Melting Technology | Dual-melt practice: Vacuum Induction Melting + Electroslag Remelting (VIM + ESR) |
| Wall Thickness Range | 5.0 mm to 25.0 mm (Custom heavy-wall profiles available) |
| Outer Diameter (OD) | 25.0 mm to 250.0 mm (Engineered to OEM drawing) |
| Machining Accuracy | CNC Turning & Boring tolerance up to ±0.005 mm (±0.0002 in) |
| Surface Roughness | Internal bore: Ra≤0.4 μm; External seal face: Ra≤0.2 μm |
| Yield Strength (Rp0.2) | ≥120 ksi (827 MPa) |
| Tensile Strength (Rm) | ≥150 ksi (1034 MPa) |
| Elongation (A5) | ≥18% |
| Hardness Range | 32−38 HRC (Homogeneous through-thickness hardening) |
| Non-Destructive Testing (NDT) | 100% Ultrasonic Testing (UT) + Liquid Penetrant Testing (PT) |
Formulated with a balanced nickel-chromium-molybdenum matrix, our corrosion-resistant Incoloy 925 precision tubular component provides superior resistance to pitting, crevice corrosion, and hydrogen embrittlement. It demonstrates zero stress-corrosion cracking in severe wet H2S and high-salinity downhole conditions.
Through optimized solution annealing and double-aging precipitation heat treatment, the alloy develops intermetallic gamma-prime (γ′) strengthening phases. This ensures our tubular components maintain yield strengths exceeding 827 MPa while preserving impact energy and fatigue resistance under cyclic hydraulic pressures.
Our computer-controlled multi-axis machining centers ensure strict concentricity, thread integrity, and micro-inch seal surface finishes across the 5mm–25mm wall thickness span. This eliminates leakage risks across flapper valves, equalizing pistons, and safety valve flow tubes.
Heavy-wall sections up to 25mm require stringent grain refinement. Our VIM+ESR refining process guarantees uniform microstructure from the outer surface to the core, preventing macro-segregation and ensuring consistent mechanical properties along the entire tubular length.
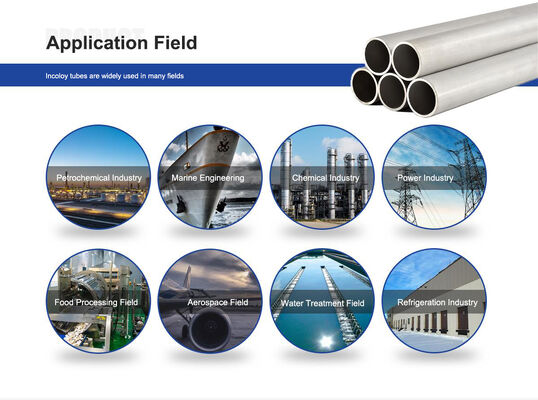
Used as internal flow tubes, hydraulic piston housings, flapper seat sleeves, and lock mandrels where zero-fail shutoff reliability is required under high-pressure differential conditions.
Essential for polished bore receptacles (PBR), expansion joints, sliding sleeves, and landing nipples operating in deep sour gas and gas condensate reservoirs.
Machined into valve stems, choke inserts, and high-pressure seat rings exposed to abrasive drilling muds, acidizing fluids, and corrosive production fluids.
Ideal for chemical injection sub-components, gas lift mandrels, and subsea landing strings where long-term corrosion fatigue and galvanic compatibility are paramount.
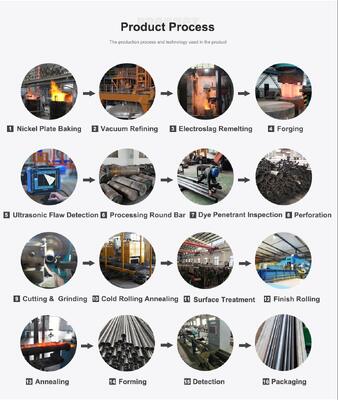
DLX controls the entire manufacturing journey from vacuum induction melting and electro-slag remelting to hot forging, specialized heat treatment, and 5-axis CNC machining. This single-source control ensures absolute traceability and batch-to-batch consistency.
With our state-of-the-art production base and extensive inventory of high-grade nickel alloy billets, DLX maintains a monthly capacity of 1,200 metric tons. This enables rapid turnaround for standard tubulars and streamlined production schedules for high-volume OEM orders.
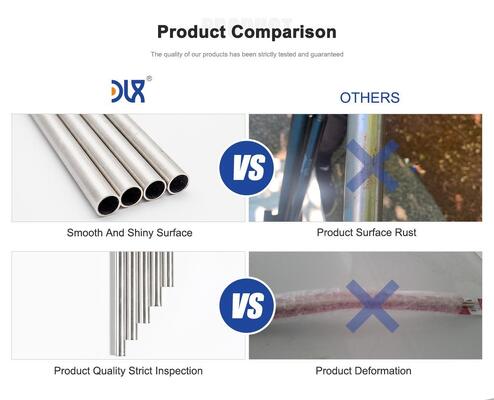
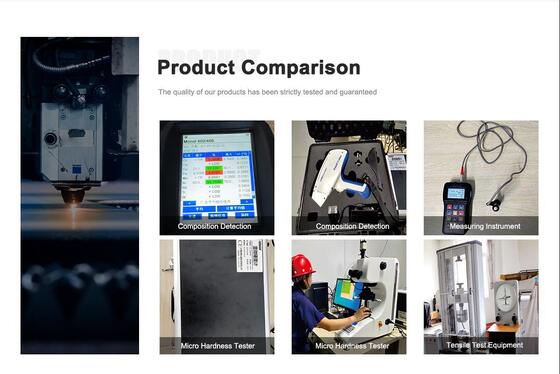
Every Incoloy 925 precision machined tubular component is subjected to rigorous quality gates, including full-length ultrasonic testing (UT), dye penetrant inspection (PT), hydrostatic pressure testing, and coordinate measuring machine (CMM) dimensional verification.
We specialize in build-to-print manufacturing. Whether you require pilot prototype batches for field qualification or continuous volume supply for safety valve production lines, we provide tailored packaging, protective end-caps, and complete material certification dossiers.
A: Conventional stainless steels and duplex alloys are susceptible to chloride stress corrosion and sulfide stress cracking when exposed to elevated temperatures and sour gas (H2S). Incoloy 925 offers a unique combination of high tensile/yield strength (via titanium/aluminum age-hardening) and superior resistance to pitting, crevice corrosion, and environmental stress cracking, making it the industry benchmark for fail-safe subsurface safety valves.
A: With our precision multi-axis CNC turning and boring centers, we routinely achieve outer and inner diameter tolerances within ±0.005 mm (±0.0002 in) and internal surface finishes as fine as Ra 0.2 μm to Ra 0.4 μm, ensuring tight fluid seals and friction-free actuation for valve pistons.
A: Heavy-wall tubulars undergo strict vacuum dual-melting (VIM+ESR) followed by high-ratio hot forging and computer-regulated solution annealing and aging. This eliminates chemical banding and guarantees uniform precipitation of strengthening phases, yielding consistent hardness (32–38 HRC) throughout the entire cross-section.
A: For custom engineered and machined Incoloy 925 tubular components, our MOQ is flexible and tailored to project requirements—supporting small pilot qualification runs as well as continuous OEM series production. Standard production lead times range from 3 to 5 weeks depending on custom wall profile and machining complexity.
A: Every delivery includes a comprehensive quality documentation package containing Chemical Composition Analysis, Mechanical & Tensile Test Data, Hardness Mapping, 100% NDT (UT/PT) Inspection Reports, and CMM Dimensional Inspection Sheets.


 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 中文
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski
